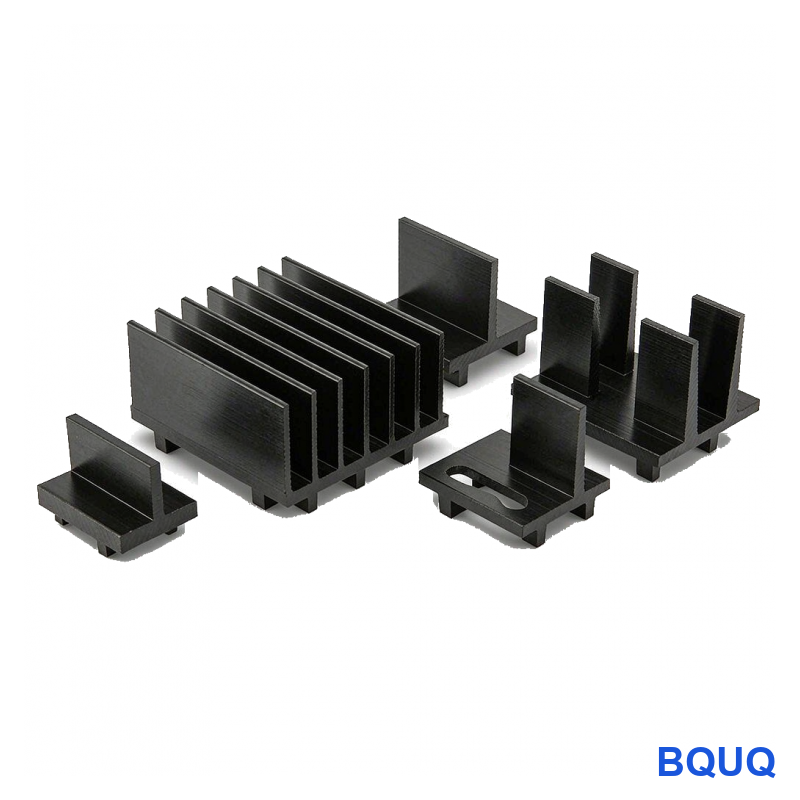
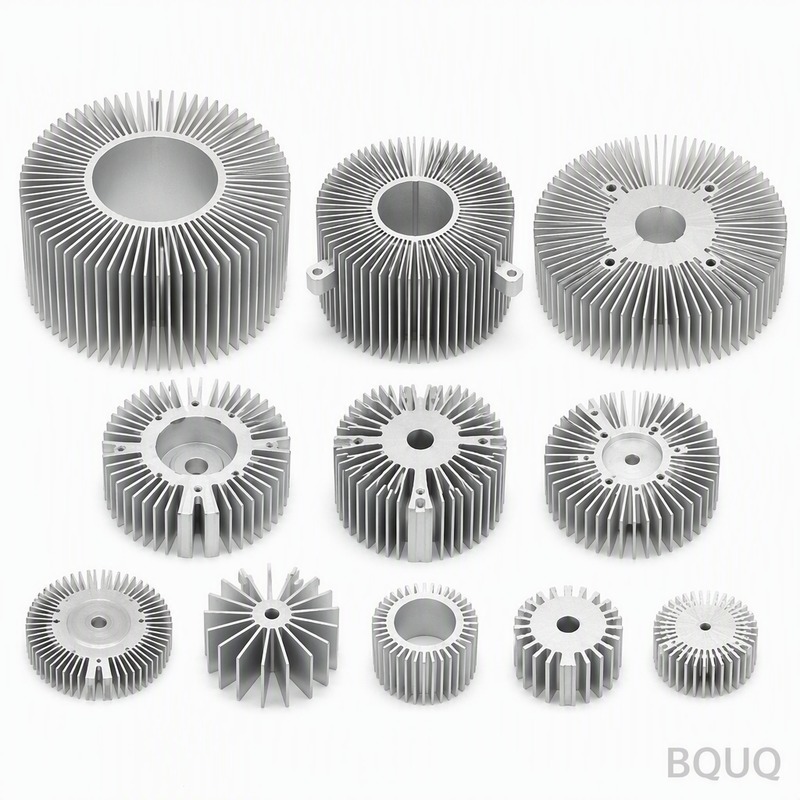
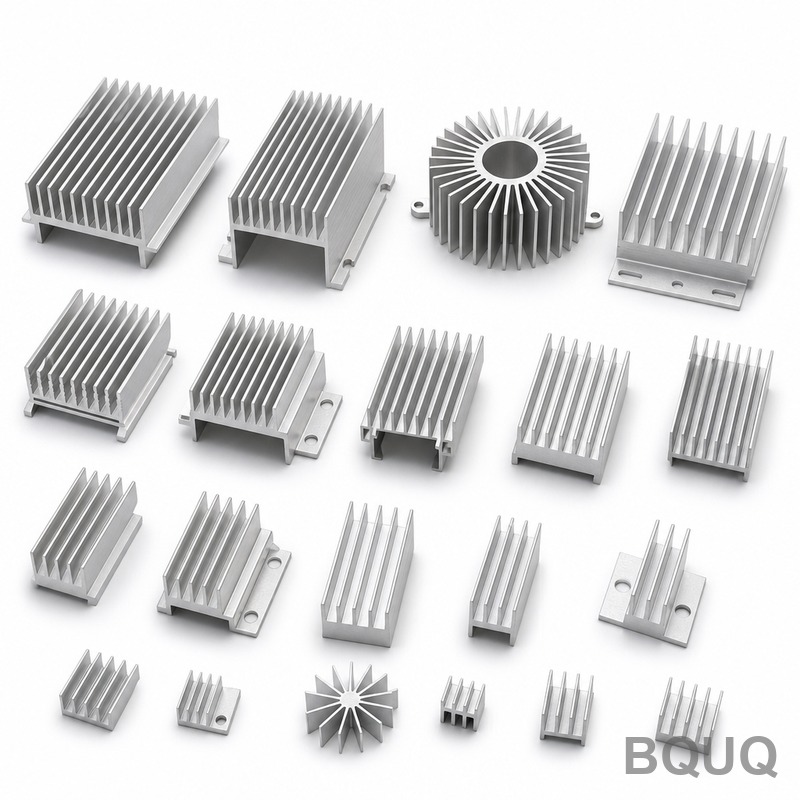
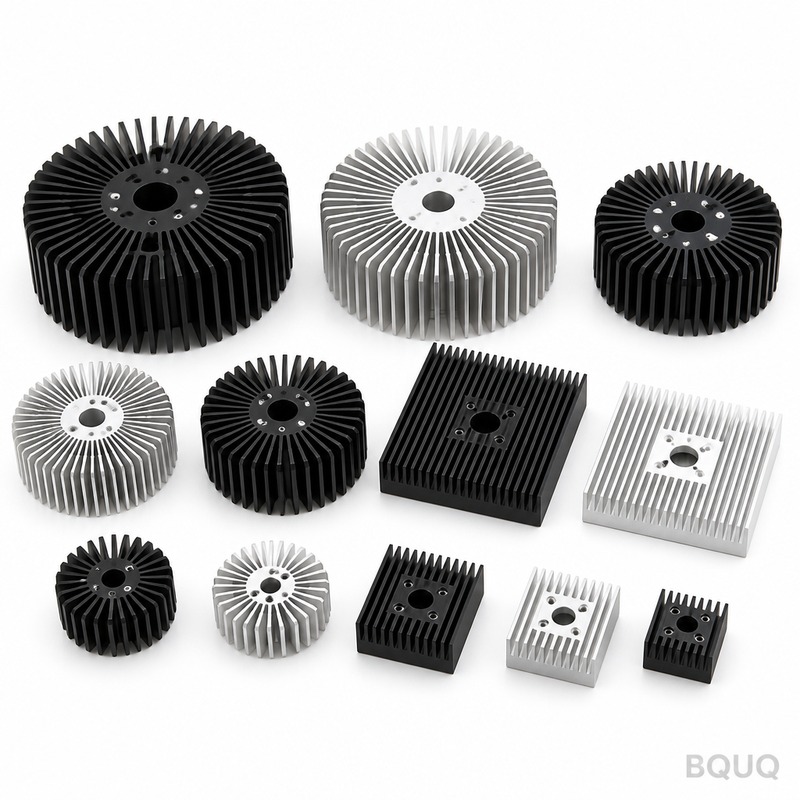
Tản nhiệt nhôm cho seeed studio xiao: 6061-T6 aluminium, 1.0 mm fins at 2.0 mm pitch, 0.05 mm over 100 mm flatness, 0.35 K/W thermal resistance. MOQ 50 pcs, ...
Tản nhiệt nhôm cho seeed studio xiao
Tản nhiệt nhôm cho seeed studio xiao: 6061-T6 aluminium, 1.0 mm fins at 2.0 mm pitch, 0.05 mm over 100 mm flatness, 0.35 K/W thermal resistance. MOQ 50 pcs, ...
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
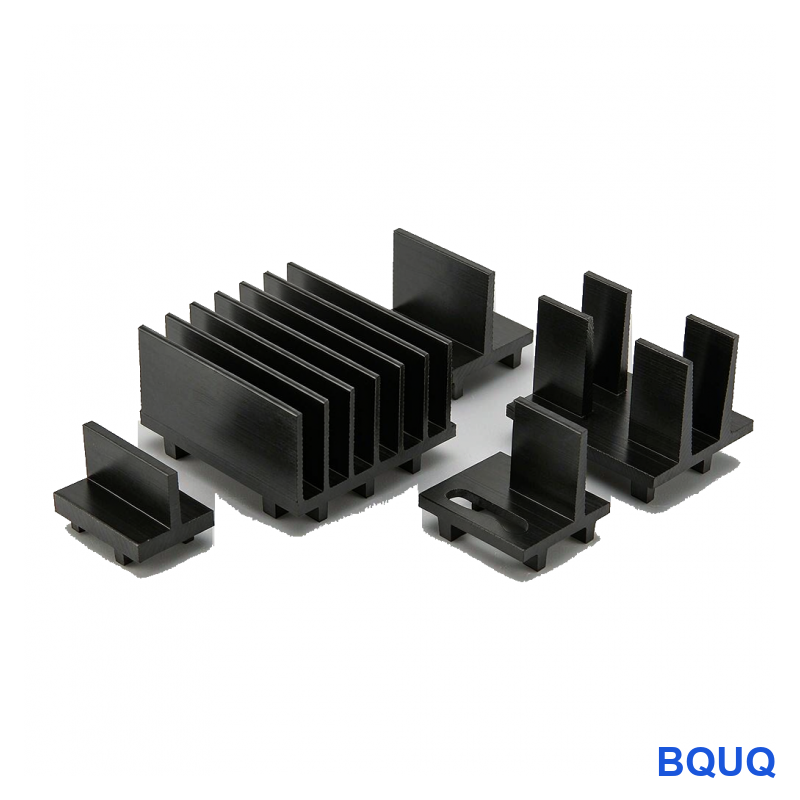
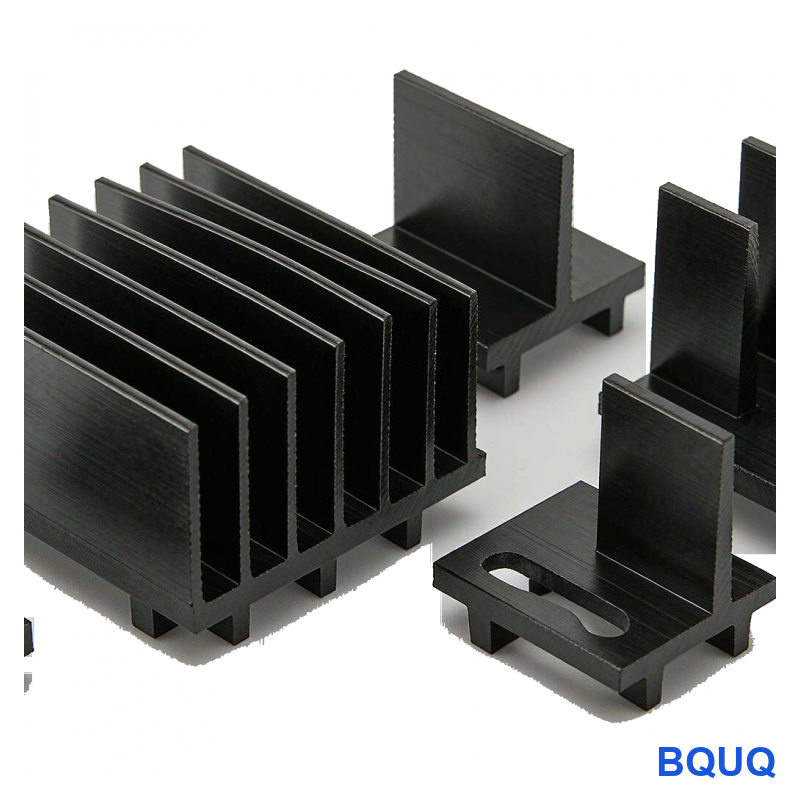
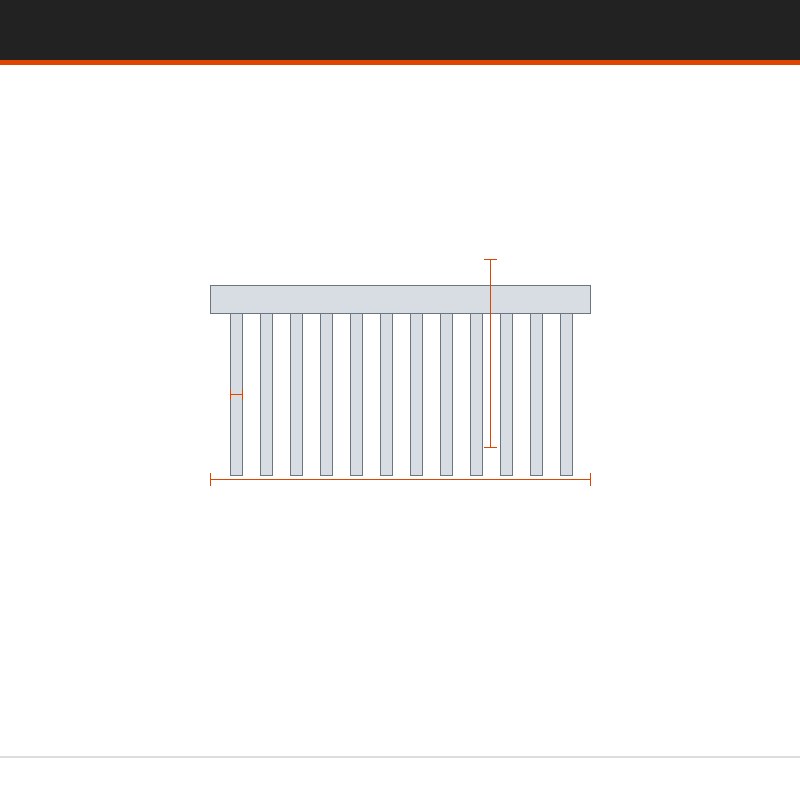
This Tản nhiệt nhôm cho seeed studio xiao covers 20 x 20 x 10 mm in 6061-T6 aluminium, with 22 mm fins at 2.0 mm pitch. Thermal performance is 0.35 K/W at ΔT = 60 K, confirmed by CMM 0.001 mm resolution, with zinc-nickel plating, trivalent passivation available.
Design Approach and Process
Stamping gives a repeatable 1.0 mm fin profile that extrusion cannot hold: the die forms every fin in one stroke, so pitch stays within ±0.05 mm across a 120,000 pcs run.
Low fin gauge is where stamping wins: 1.0 mm fins at 2.0 mm pitch give more surface per cubic millimetre than a machined or extruded profile of the same envelope.
Stamped construction tolerates batch variation better than extrusion: die wear shows up first as a measurable shift in fin pitch, which inspection catches at CMM 0.001 mm resolution rather than in the field.
Pressing 6061-T6 aluminium keeps the Tản nhiệt nhôm cho seeed studio xiao light, from 280 g depending on envelope, without sacrificing fin density, which matters where airflow path length is already fixed by the enclosure.
Every stroke is dimensionally identical, so ±0.10 mm hole position carries across the batch. That is what makes EV and OBC charger volume programs repeatable.
Material Selection and Surface Finish
The standard material is 6061-T6 aluminium, supplied with zinc-nickel plating, trivalent passivation. For applications where EV and OBC charger exposure is a concern, we recommend the passivated route; where conductivity matters more than weight, copper C110 raises thermal performance and roughly doubles unit mass.
Tolerance Classes You Can Specify
General dimensions run to ±0.10 mm, with critical features such as ±0.03 mm on fin pitch held separately. Formed geometry inherits tooling repeatability of ±0.05 mm, and hole position is held to ±0.10 mm. Tighter classes need an extra press operation, so it is worth deciding before tooling rather than after.
Sampling is AQL 0.65 for critical dimensions and 1.5 for general, with CMM 0.001 mm resolution on every first article. Deviations beyond ±0.10 mm trigger a full-lot sort.
Lot traceability runs from coil to carton: heat number, press stroke range and inspection record stay attached, so a field issue can be tied back to a specific run.
Flatness is measured on granite rather than on cast iron, because 0.05 mm over 100 mm at 20 x 20 x 10 mm reads differently on a plate that has not been lapped. Records keep both readings.
We inspect 1.0 mm fin tips for burr and crack after forming, because stamping can split a root without shifting any drawing dimension. Burr limit is set per part.
In EV and OBC charger, the 0.35 K/W rating determines how much airflow the enclosure still needs. At EV and OBC charger junction temperatures, 1.0 mm fins at 2.0 mm pitch keep the delta-T inside the sensor budget.
EV and OBC charger customers typically specify 6061-T6 aluminium for corrosion reasons and then hold the drawing to ±0.10 mm. The 120,000 pcs line absorbs the volume without a second source.
EV and OBC charger packaging and vibration rules push toward one-piece construction. A stamped Tản nhiệt nhôm cho seeed studio xiao has no adhesive to creep, which is the usual failure mode in two-part coolers.
In EV and OBC charger, the base usually doubles as the mounting interface. 1.5 mm with 0.05 mm over 100 mm flat gives a stable surface for the EV and OBC charger thermal pad.
Every lot is inspected with CMM 0.001 mm resolution, and the report is included in the shipment. We check 0.05 mm over 100 mm, 2.0 mm, 1.5 mm and hole position against ±0.10 mm. Lot traceability from coil to carton is kept for 10 years.
What tolerance can you hold?
General dimensions run to ±0.10 mm; critical ones such as ±0.03 mm on fin pitch are held separately. Formed features inherit tooling repeatability of ±0.05 mm. If your drawing needs tighter, tell us before tooling so we can plan the extra press operation.
Do you test for thermal resistance?
We test at ΔT = 60 K, natural convection and report 0.35 K/W. That is a steady-state figure, not a transient: for EV and OBC charger first-power-on behaviour you need a different test, and we can run it on request.
Is there any risk of the fins bending in transit?
With 1.0 mm fins and standard PE bag + export carton, 20 kg per carton, damage is rare. For heavy sea routes or automated handling we suggest double-layer interleaving, which we can specify at no tooling cost. We have shipped 120,000 pcs per month this way without a transit claim in the last 3 years.
Can you help with thermal simulation before sampling?
Yes. Send your enclosure airflow, inlet temperature and the heat load to be dissipated, and we will run a steady-state model and return a suggested 1.0 mm and 2.0 mm combination. That usually saves one tooling iteration.
How We Manufacture and Ship
The line sits in Dongguan in a single ISO9001 plant. 160 T presses cover the Tản nhiệt nhôm cho seeed studio xiao family, and 120,000 pcs per month is current committed output.
Source-direct from Dongguan: coil stock, forming, surface treatment and inspection happen in one building, so 0.05 mm over 100 mm flatness is verified before the part is packed.
The factory holds ISO9001 and can ship RoHS and REACH documentation with the PE bag + export carton, 20 kg per carton. Third-party SGS inspection is arranged on request before the container is sealed.